


Table of Contents
Case Study Overview
MGS Manufacturing is a long-time customer of Tantec, and throughout the years many Tantec systems have been deployed for MGS customers as part of unique medical applications. MGS uses Tantec LeakTEC tools for leak testing and detection, identifying micron holes in the products produced.
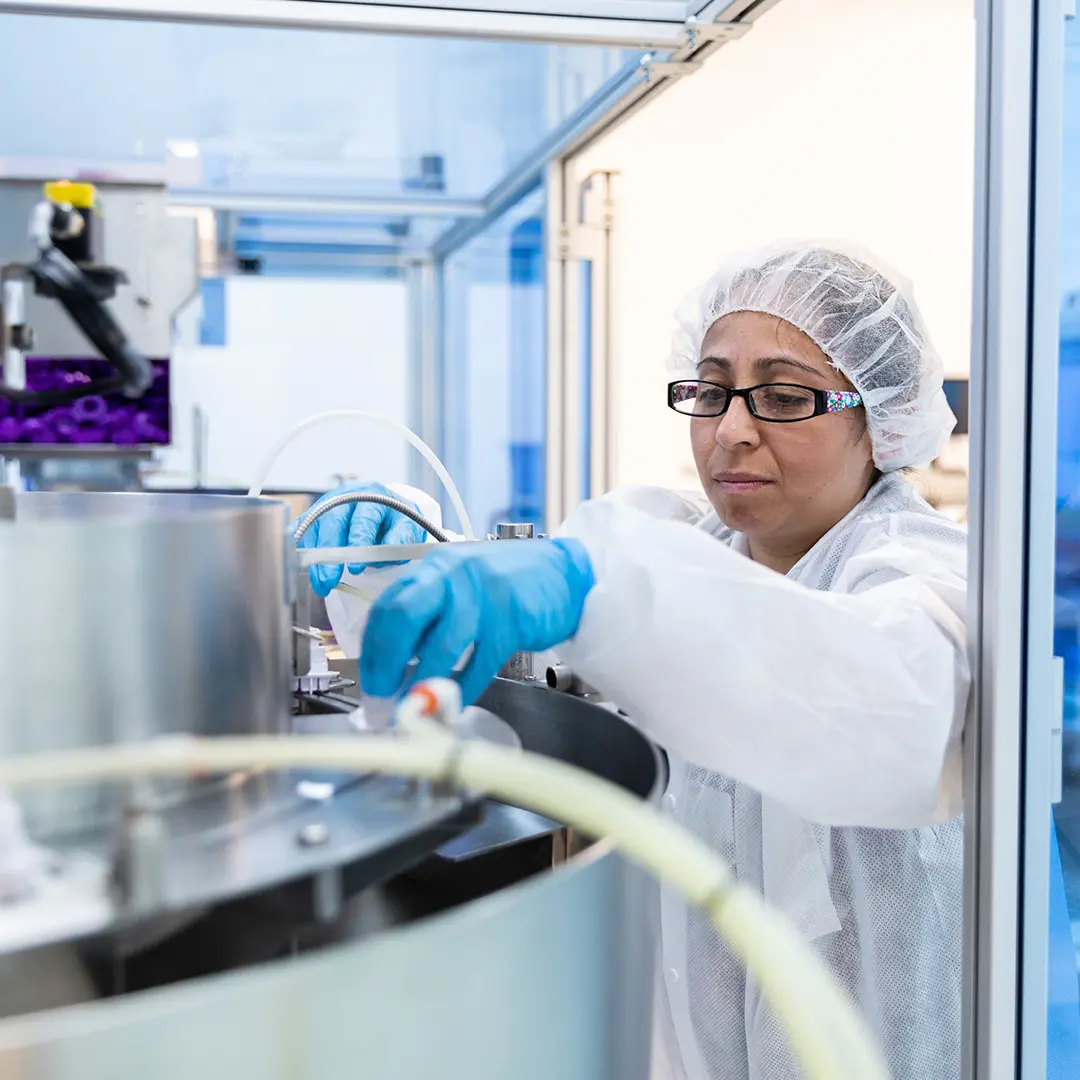
There are a number of leak detection methods on the market, each with their own advantages and disadvantages. Using high voltage leak detection has it’s strength in detecting holes in moulded polymer parts that have an accessible area to present a probe.
If the part suits the process, the process is incredibly quick, repeatable and sensible. 100% testing can be achieved, inline with automation and without the need for process gases or consumable parts.
The Problem
Holes in moulded components might be important to detect and this is often the case in medical devices or pharmaceutical containers. It’s also common to detect and avoid defect issues in products that can be ruined if exposed to air, such as food and drink.
Leaks inward tend to be the problem in many of these applications, with bacteria, viruses and air being able to get in to the packaging and spoiling the product. But it may also be leaking of the product to the outside world, especially if it’s dangerous.
Ensuring the packaging and product leave the factory in a safe and satisfactory state to meet product shelf life and avoid risks due to contamination or complaints and brand issues can be a very serious and important issue.
Possible Solutions to Leak Detection
There are a number of solutions on the market, and many have their niche and advantages.
Helium or gas detection leak testing is often a fantastic tool for finding holes in irregular or large shaped parts. This method usually isn’t specific to individual materials or applications either and so can be quite flexible. The technology works by having a gas that can be detected in minute amounts by an external probe. The gas molecules are so small that they can escape through even the tiniest of holes and because the inside of the vessel is usually pressurised, this helps push out gases and find holes more efficiently.
This can be a quick method, but it can take minutes. It also requires specific gases and probes that are needed for every test as well as needing a controlled environment to test in.
Other leak detection tests may work on pressure changes over time and will work with a positive and negative pressure arrangement which in the case of a good part would stay stable, while in a damaged part would see the vacuum, negative pressure increase over time. Like gas detection, this can be a very useful tool for larger or complex parts and material type will likely not make a big difference. Time however can be long and testing 100% of parts in line would be very difficult for many applications.
High Voltage Leak Detection
The idea behind these systems is quite simple, it’s all about detecting when high voltage makes a direct, unrestricted path to ground. At high voltages the electricity can find a path to ground over several centimetres so it will find a hole, go through it and we detect this as there’s no resistance in the circuit – we have an electrical arc.
If the part is good on the other hand, there is resistance in the circuit and the power will not make a direct arc.
This has been done on a less technical scale for many years with the use of holiday detectors for pipes. The Tantec LeakTEC system is a much more accurate, engineered solution, commonly designed for integration into automation for high speed lines such as medical components being tested after injection moulding.

This method is extremely quick and offers 100% testing of parts, but comes at the cost of having to be a component that can have a probe placed within the part to create a circuit. A cap or lid is perfect for this, while a complex assembly will likely have too much geometry to make it work sensibly.
MGS Manufacturing Approach
With the various systems available, it’s sensible to evaluate each one for the specific components requiring testing.
Shawn Krenke, CTO and Senior Vice President of Automation at MGS considers the different techniques.
“When you deploy a pressure decay type leak test, you need to create a seal against the part, you need to fill the part with air and then need to stabilise for a given amount of time before you can evaluate for a leak”
“With pressurized testing, you are more vulnerable to false failures as your seal starts to deteriorate against the part. The leak might be between your testing seal and the product you’re testing, which is not optimal.”
For high-voltage leak testing, you don’t have to create a perfect seal, you don’t need to touch the component with the test probes at all making it a non contact test method. High-voltage testing can test for much smaller pinholes than other testing methods can, and at speeds no other testing setup can match.
“Your test time with the other methods becomes very long to get the resolution required. Additionally, sometimes with pressure testing your environment may need to be precisely controlled for the sensitivity to accurately find the defects your testing for” Krenke explains, and continues:
“With high-voltage testing, we can detect very small micro-holes in parts. We are effective down to about two microns. High voltage is accurate for even smaller holes, but that is more than adequate to satisfy the test requirements for our current applications .”
A lot of the products MGS produces are high-volume. This means that cycle times need to be fast.
“We require a technology that can be done or conducted in a very short time-frame. With for example reagent strips that we produce we are testing five features on each part, and we are testing them right beside our 8-cavity moulding press that is producing the parts,”
“So, there’s basically 40 different unique areas that we’re testing with each cycle when we’re making those eight parts. And the cycle of the testing only takes about 1 second. Testing for 40 characteristics i 1 second is only achievable with a LeakTEC solution.”
In practice, MGS puts the eight parts onto a pallet that has test probes underneath it. Then they can move the pallet underneath another set of fixed electrodes. They energize the system in a matter of milliseconds and then they are made aware of any leaks detected in those 40 areas.
Krenke clarifies: “This is all an automatic process, where a robotic arm both loads the test fixture, waits until the test is done and then separates the nonconforming product from the good parts.”
LeakTEC Proved to Have a Short Return on Investment
With the high production volume and the need to test 40 potential failure points, MGS has found the LeakTEC solution to be a good investment.
“When you, like us, need to test lots of areas it doesn’t matter if you are only testing for one point of failure instead of 40 — the costs will not be exponentially 40x like it could be for independent pressure decay channels. On a one-off test basis, air might be slightly less expensive than high voltage, but it quickly goes the other way when you’re looking at more than once characteristic.”
While the cost of automating a system like this does have an initial cost, the running and maintenance costs of the systems are very low – often only a few hundred watts of power needed, and only when the tests are being conducted which is often less than three seconds.
This along with the fact that entire batch testing can be done inline reducing real world failures and recalls can mean a significant financial saving.
Working with another customer, their original test method had been to pressure test multiple components at set times of day – start of batch, during first hour, during second hour etc.
If they found any defect in the component they tested, they scrapped all components that had been produced since the last test. This was a multi cavity tool producing thousands of parts an hour and the waste was high. The risk was also fairly high as such a low number of parts were tested.
Introducing LeakTEC gave them entire batch testing so they could remove a single row of components if a failure was found – losing four components rather than hundreds or thousands.
Learning More About Leak Detection
Follow the links below to find out more, there’s also a quick video as an introduction to the technology on the introduction page.
These systems are always built to meet the specification of the part, this doesn’t mean they can’t be redeployed or used in multiple areas, but the end tooling is specific to the part. Our lab here can run Leak Detection testing using simple tooling to prove the technology and find micro holes in components – we’re always keen to put the system to the test if you want to send samples our way!


